Stainless steel (such as SS 304 and SS 316) offers superior corrosion resistance, withstands aggressive chemical washdowns and sterilization agents, and prevents contamination in cleanroom environments.
Machine Guarding Solutions for Pharmaceutical Manufacturing
- Swiza Safetech
- September 28, 2026
- Views Count
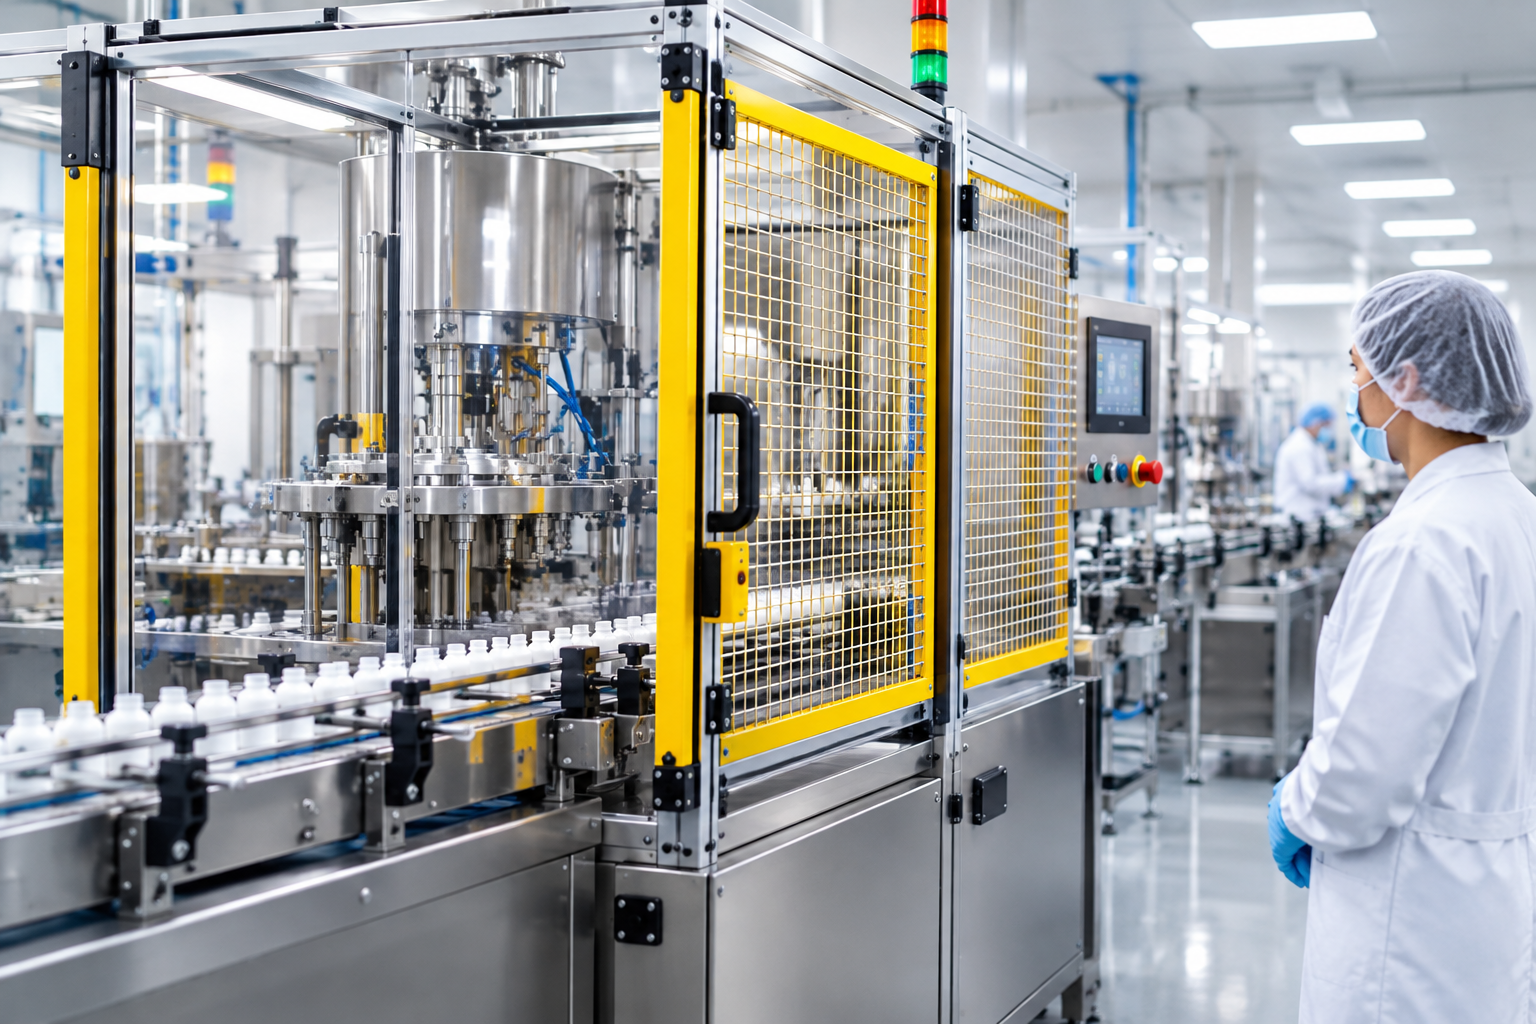
Pharmaceutical manufacturing environments require strict adherence to hygiene standards, precise regulatory compliance, and robust operator safety. High-speed packaging lines, tableting machines, blenders, and automated processing equipment demand specialized machine guarding solutions designed to prevent accidental contact while maintaining cleanroom integrity.
In this guide, we explore the essential requirements, design features, and benefits of implementing advanced machine guarding systems in pharmaceutical manufacturing facilities.
Why Machine Guarding Is Critical in Pharma Plants
Unlike standard heavy industrial settings, pharmaceutical production facilities deal with sensitive compounds, sterile environments, and rigorous validation protocols (such as GMP and ISO 14120). Effective machine guarding protects operators from moving mechanical parts, pinch points, and automated robotic arms while ensuring zero contamination of pharmaceutical products.
Key Objectives:
- Prevention of mechanical and entrapment injuries
- Compliance with ISO 14120 safety standards for fixed and movable guards
- Maintenance of sterile cleanroom airflow and particulate control
- Seamless integration with interlock safety switches and light curtains
- Easy access for cleaning, sanitization, and maintenance
Essential Features of Pharma-Grade Machine Guards
Machine guards deployed in pharmaceutical and cleanroom environments must possess specific material and design characteristics.
Recommended Specifications:
- Corrosion-Resistant Materials: High-grade stainless steel (SS 304 / SS 316) or powder-coated aluminum to withstand frequent chemical washdowns and sterilization.
- Smooth Surface Finishes: Crevice-free designs to prevent dust accumulation and bacterial growth.
- Clear Visibility Panels: Polycarbonate or laminated glass inserts that allow operators to monitor active processes safely without opening enclosures.
- Modular Flexibility: Prefabricated modular panels that allow quick reconfiguration during line upgrades or machinery retrofitting.
Ideal Applications: Blister packaging lines, capsule filling machines, granulation suites, and automated inspection systems.
Integration with Safety Interlocks and Automation
Modern pharmaceutical manufacturing relies heavily on automation. Machine guarding systems cannot act as mere physical barriers; they must interface seamlessly with safety control architectures.
Integration Standards:
- Safety Interlocks: Tongue or RFID-coded safety switches that immediately halt machine operation if a guard door is opened.
- Light Curtains & Scanners: Electro-sensitive protective equipment used alongside physical fencing for access points requiring frequent manual intervention.
- Emergency Stop Integration: Easily accessible E-stop buttons wired into the primary safety PLC.
Benefits of Modular Safety Fencing in Pharmaceutical Units
| Feature | Traditional Guarding | Modular Safety Guarding |
|---|---|---|
| Installation Time | Slow, requires custom on-site welding | Fast, bolt-together modular assembly |
| Cleanroom Compatibility | Variable, prone to corrosion | High, available in SS 304 & sealed profiles |
| Flexibility | Rigid, difficult to modify | Easily expandable or reconfigured |
| Compliance | Dependent on custom fabrication | Certified to ISO 14120 / CE standards |
Conclusion
Investing in high-quality machine guarding solutions is indispensable for pharmaceutical manufacturers aiming to safeguard their workforce, comply with stringent global safety regulations, and maintain sterile production environments. By choosing certified modular fencing and stainless steel enclosures, pharma plants achieve long-term operational reliability and uncompromised safety.
FAQs
-
Why is stainless steel preferred for pharma machine guarding?
-
Are Swiza machine guarding systems compliant with ISO 14120?Yes. All safety fencing and machine guarding systems manufactured by Swiza Safetech comply with ISO 14120 general requirements for the design and construction of fixed and movable guards.
-
Can machine guards be customized for specific pharma machinery?Yes, Swiza Safetech provides fully customized modular machine guarding solutions tailored to the exact dimensions, access requirements, and interlock specifications of your pharmaceutical equipment.